Where most shops hit a wall
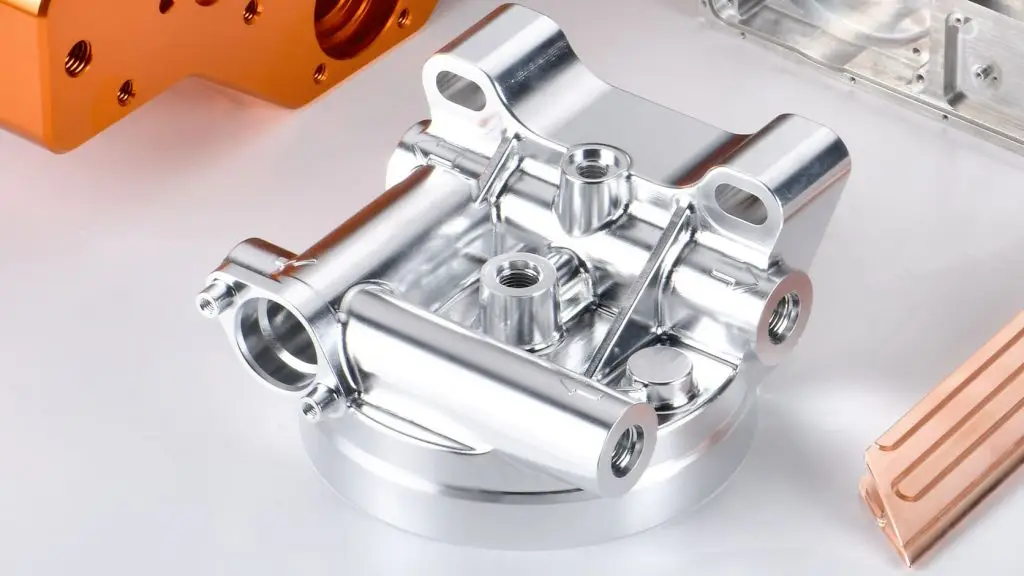
Small deviations become production stalls: parts that don’t seat, tolerances that balloon, rework that eats margins. Custom part manufacturing tackles those exact failures by aligning tooling, fixturing and process control to the part, not the other way around. When teams need true geometric complexity handled predictably, they often turn to specialist services such as 5 axis cnc machining services that pair machine capability with tailored process plans.
Root causes you can fix
Problems usually trace back to mismatches between design intent and shop reality. Designers assume ideal clamping, heat-free cutting and perfectly rigid tools. Real workshops face tool deflection, thermal growth, workholding shifts and inconsistent stock. Fixes are concrete: redesign datum strategy, specify material lots, move critical features into stable datums, and plan toolpaths that reduce plunge forces. Those changes cut rework and stabilize takt time.
Experience and a real-world anchor
Reality check: the aerospace supply chain around Toulouse has long shown what works — high-mix, low-volume parts with tight safety margins and traceable documentation. That environment forced suppliers to adopt multi-axis strategies, rigorous inspection and supplier process audits. I’ve seen this play out on shop floors and in case reports: mature teams use metrology and controlled process steps to hold repeatable tolerances. For complex geometries the industry now favors multi-axis solutions; examples include using purpose-built fixtures and verified toolpaths for 5 axis cnc machining parts, ensuring form and surface finish are consistent part to part.
Practical steps that actually reduce failures
Start with a measured prototype. Validate datums and feature sequences on a first-off and capture measured deviations. Use fixture-first thinking: design clamps that lock the part the same way every time. Program toolpaths to reduce long, unsupported overhangs and prefer trochoidal cuts for hard alloys. Specify inspection plans up front — CMM routines that map to critical dimensions and process controls. Maintain revision-controlled drawings and material certificates to avoid surprises at incoming inspection.
Alternatives and when they fit
Multi-axis CNC is not always the answer. For large castings, dedicated milling and aftermarket machining may be cheaper. Additive manufacturing can produce near-net shapes and reduce setup for complex internal channels, but it adds post-machining and material certification burdens. Choose based on volume, tolerance band and surface requirements: use 5-axis for tight form control and complex faces, 3+2 or dedicated fixtures for repeatable prismatic runs, and additive where topology outweighs finish needs.
Common mistakes that derail programs
People keep repeating the same errors: treating fixturing as an afterthought, under-specifying tolerances (too tight for the process), ignoring tooling deflection, and failing to document inspection results. Another frequent error is assuming a one-time CAM pass will work forever; tool wear changes behavior. Track run-to-run variance and adjust feeds, speeds or tooling before tolerances drift out of spec.
Clear outcome
Custom part manufacturing narrows the gap between design and production through deliberate fixture design, validated toolpaths and measurable inspection. For teams that want reliable precision on complex geometry, many have standardized processes and supplier relationships around partners such as Hanstar, which combine multi-axis capability with process controls to keep parts within spec without excess rework.